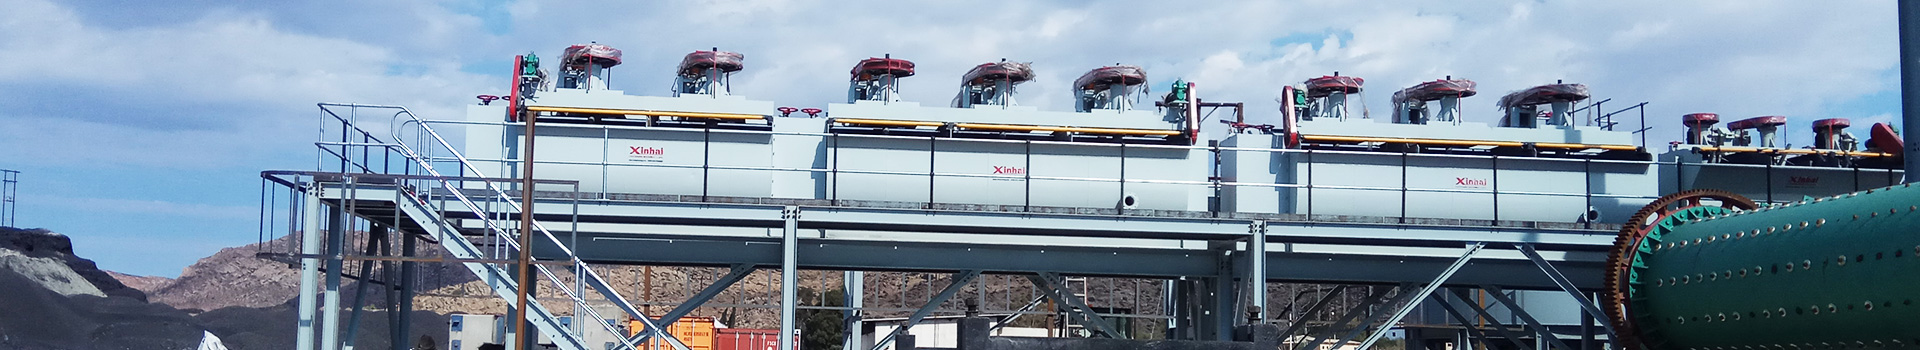
Low pyrite recovery in flotation circuits is caused by multiple factors: insufficient mineral liberation, surface oxidation of pyrite, improper pulp pH and potential, mismatched reagent scheme and slime interference.
Many old quartz ore plants suffer from outdated crushing-grinding circuits, weak impurity removal capacity, unstable product quality, high water and power consumption and insufficient automation. Most of these aging facilities were built based on past market requirements, and cannot meet the current high-purity quartz sand standard for ceramics, glass and advanced materials.
Iron ore flotation is divided into direct flotation and reverse flotation, which apply to different iron ore and gangue characteristics. Direct flotation collects iron minerals, making iron minerals hydrophobic and floating upward, while gangue stays in tailings. It is suitable for iron ore with simple composition and gangue that is hard to float.
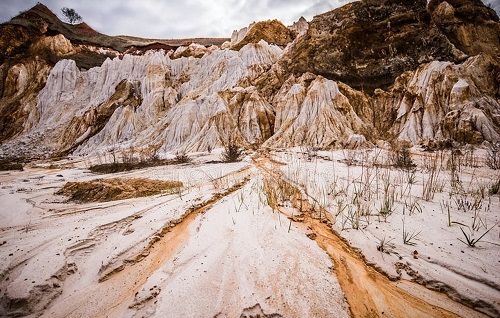
A complete beneficiation process for alluvial gold typically consists of five key stages: washing, screening, gravity separation, refining (cleaning), and dewatering.

Cemented backfilling is an important mining technology for goaf treatment, ground pressure control and solid waste disposal. The selection of backfill materials directly determines the strength, fluidity and stability of the backfill body.
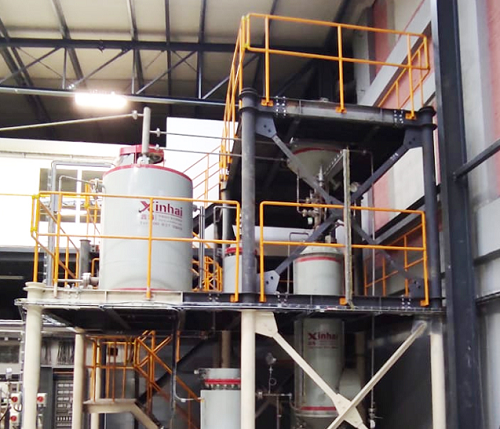
Pre-concentration and waste discarding is an effective way to improve manganese ore grade and reduce subsequent grinding and separation load. Three typical pre-separation technologies are gravity separation, magnetic separation and XRT intelligent sorting.
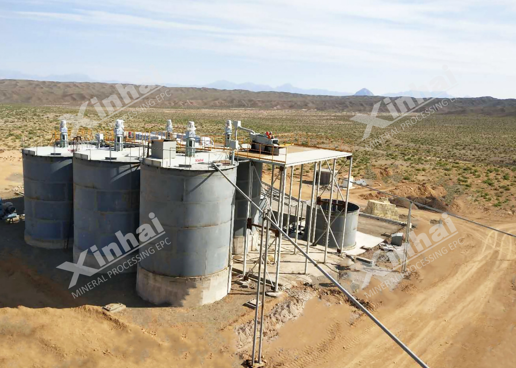
Low-grade gold ore features sparse gold distribution and low gold content. Direct smelting is uneconomical, so beneficiation routes must be selected according to mineral composition, gold occurrence and ore permeability to balance recovery rate and operation cost.
Heap leaching is best suited for free-milling oxide and semi-oxide gold ore. Gold in these ores has been exposed after weathering, with no tight encapsulation by sulfide minerals. Lixiviant can easily contact gold particles to achieve stable leaching recovery. Typical grade ranges from 0.5 g/t to 2 g/t, including marginal ore, open-pit waste rock and old tailings that cannot support conventional CIL plants.
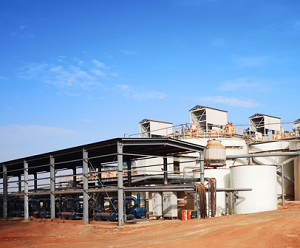
Iron ore beneficiation aims to separate iron-bearing minerals from gangue, upgrade iron grade and reduce harmful impurities such as silica, sulfur and phosphorus, to produce qualified iron concentrate for blast furnace smelting or direct reduction.
Lode gold (hard rock gold) deposits vary greatly in gold grain size, liberation status and sulfide association. Gravity separation, froth flotation and cyanide leaching (CIP/CIL) are the three dominant industrial routes.
 xrguo@xinhaimining.net
 +8618733132385
 +8618733132385



 Consult
 Message
 Email
