 xrguo@xinhaimining.net
 +8618733132385
 +8618733132385


Silver Concentrate Quality Control and Recovery Improvement in Flotation
2026-11-21 Xinhai (11)
2026-11-21 Xinhai (11)
If you have any questions, please contact us through the following ways, we will give you more and better assistance!
Most silver resources exist as associated minerals in copper, lead, zinc and polymetallic sulfide ore, and independent silver ore is relatively rare. Froth flotation is the dominant beneficiation method to enrich silver-bearing sulfide minerals such as argentite, tetrahedrite and galena. Silver flotation relies on the surface hydrophobic difference between silver minerals and gangue. After grinding and dissociation, selective collectors and regulators are added to make silver sulfide minerals attach to air bubbles and form froth concentrate, realizing high multiple enrichment of silver metal.
Ore crushing and closed-circuit grinding create the premise of flotation. Raw ore is crushed and ground to proper fineness so that silver minerals are fully liberated from gangue and associated sulfide minerals. Over-grinding produces excessive fine slime, which deteriorates flotation selectivity and causes silver loss in tailings; insufficient grinding leads to locked particles and low recovery. The grinding circuit cooperates with hydrocyclone classification, and coarse particles return to the ball mill for regrinding to keep stable particle size of flotation feed.
Slurry conditioning and reagent selection are the core of silver flotation. Commonly used collectors include xanthate, dithiophosphate and thionocarbamate, selected according to silver mineral species and associated sulfide composition. Frother such as MIBC or terpineol oil is added to form stable froth. Regulators adjust pulp pH and suppress gangue or interfering sulfide minerals. For oxidized silver ore, sulfidizing agents are added to modify mineral surface and restore floatability before flotation. The reagent dosage sequence and conditioning time directly affect silver concentrate grade and recovery.
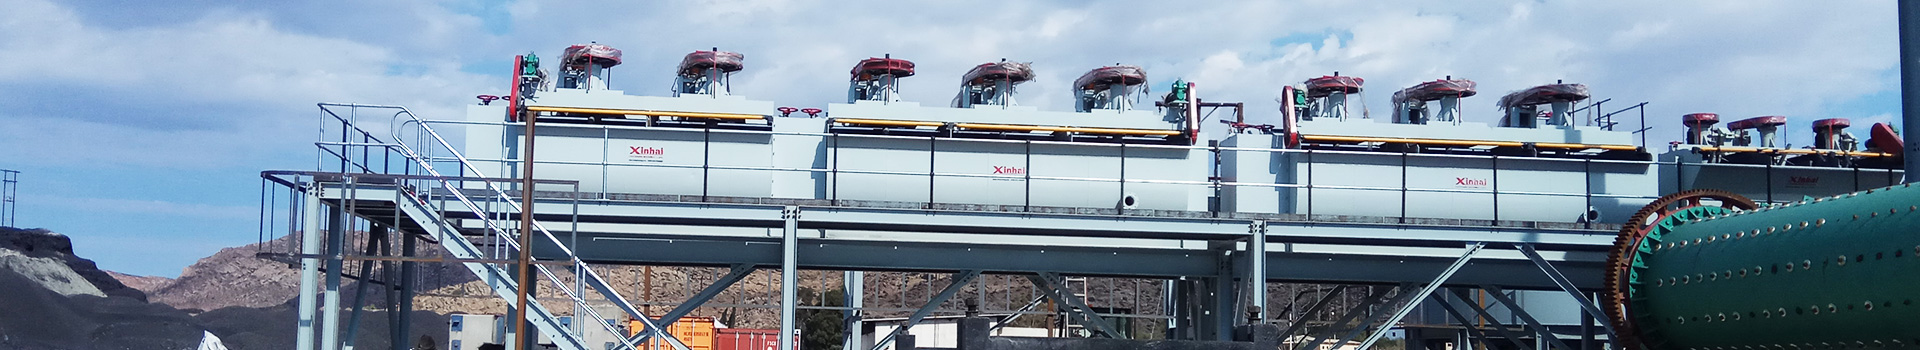
The flotation circuit generally adopts rougher, scavenger and cleaner configuration. Rougher flotation produces rough silver concentrate, scavenger flotation recovers silver minerals from rougher tailings to raise total recovery, and multiple cleaner flotation improves silver concentrate grade. If silver is associated with lead and zinc, preferential flotation is adopted to separate lead concentrate with silver, zinc concentrate and tailings step by step. Bulk flotation is suitable for simple silver-bearing sulfide ore to get bulk concentrate first, then separate valuable minerals.
Subsequent processing and optimization directions. Silver flotation concentrate can be sent to smelting directly, or combined with cyanide leaching to further extract silver. Fine silver mineral recovery is a difficult point. Fine bubble flotation and carrier flotation technology can reduce fine silver loss. Process mineralogy analysis helps identify silver occurrence state and optimize reagent system. We provide silver flotation test, circuit transformation and reagent optimization service for associated silver mines and independent silver ore concentrators


 Consult
 Message
 Email
